Engineered specifically for insulated process lines and steam headers, our Stainless Steel Lagging Extension Gauge Root Valves feature an elongated process shank (typically 4" to 6" lagging extension) that safely penetrates thermal pipe insulation cladding. Rated up to 6,000 PSI (414 Bar) with multiport block, bleed, and calibration ports, they provide safe, bubble-tight isolation and thermal standoff for pressure transmitters and gauges without damaging insulation jackets.
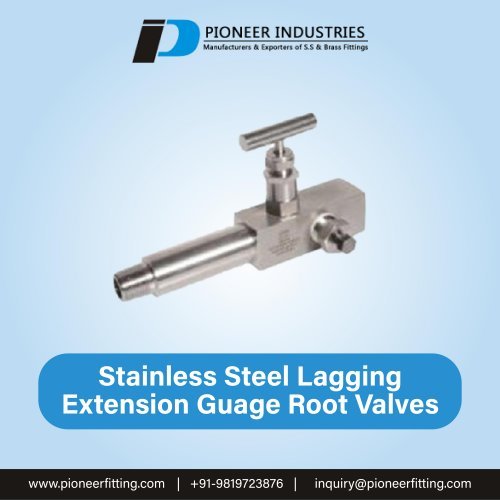
The Stainless Steel Lagging Extension Gauge Root Valve features a solid forged body with an extended process neck designed to pass cleanly through pipeline and vessel insulation lagging. In high-temperature steam headers, cracker units, and refinery piping, standard gauge valves become buried underneath thermal insulation, causing seal overheating and rendering isolation handles inaccessible. The lagging extension design solves this problem by providing a physical thermal standoff.
Combining the functions of an extended pipe nipple, process tee, primary isolation valve, and instrument vent/bleed port into a single compact forged body, this valve eliminates up to 5 potential threaded leak paths. With three 1/2" Female NPT instrument/vent outlets, technicians can simultaneously mount a pressure gauge, differential transmitter, and calibration bleed plug for in-situ testing.
Manufactured by Pioneer Industries Mumbai, our Lagging Extension Gauge Root Valves are trusted across power generation, petrochemical, and oil & gas refining facilities in over 85 countries.
Each valve is precision CNC-machined from ASTM A182 Grade F316/F316L stainless steel forgings or ASTM A479 316 bar stock. Standard non-rotating hardened stem tips prevent seat galling, while high-temperature Grafoil packing withstands extreme process conditions up to 1,000°F (538°C).
To Get Quotes within hour Call Us at 9821023876 or Send Enquiry for the products you requires
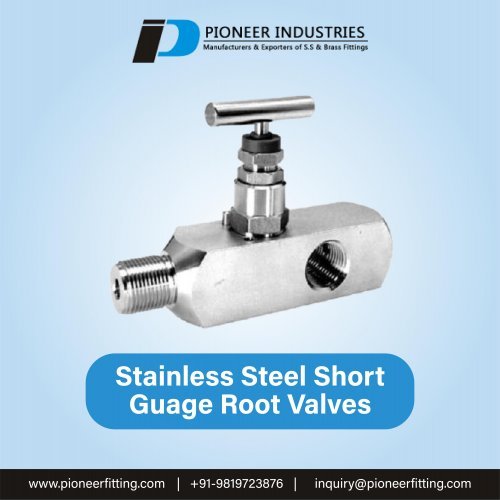
Pioneer Industries supplies precision-engineered Stainless Steel Lagging Extension Gauge Root Valves constructed with heavy-wall forged bodies designed to withstand high operational pressures and mechanical pipe vibration.
The extended shank allows easy installation through hot pipe insulation cladding, while safety bonnet lock pins prevent accidental disassembly during operational valve cycling in high-pressure service.
Extended shank lengths 4" to 6"; 1/2" & 3/4" Male NPT process inlet x (3) 1/2" Female NPT instrument outlets; 6,000 PSI at 200°F (4,000 PSI at 500°F); ASTM A182 F316/F316L.
Explore standard engineering dimensions for 1/2" and 3/4" Lagging Extension Gauge Root Valves, Operating Parameters, and Certified Metallurgy. Manufactured according to ASME B16.34, API 598, MSS-SP-99, and international instrumentation standards.
| Part No. | Process Inlet | Instrument Outlets | Lagging L1 (mm) | Overall L (mm) | Height H (mm) | Hex Body (mm) | Working Pressure |
|---|---|---|---|---|---|---|---|
| PI-GRV-LE-08M08F-4 | 1/2" NPT Male | (3) 1/2" NPT Female | 102 mm (4.00") | 184 mm (7.25") | 89 mm (3.50") | 32 mm (1.25") | 6,000 PSI |
| PI-GRV-LE-08M08F-6 | 1/2" NPT Male | (3) 1/2" NPT Female | 152 mm (6.00") | 235 mm (9.25") | 89 mm (3.50") | 32 mm (1.25") | 6,000 PSI |
| PI-GRV-LE-12M08F-4 | 3/4" NPT Male | (3) 1/2" NPT Female | 102 mm (4.00") | 190 mm (7.50") | 89 mm (3.50") | 32 mm (1.25") | 6,000 PSI |
| PI-GRV-LE-12M08F-6 | 3/4" NPT Male | (3) 1/2" NPT Female | 152 mm (6.00") | 241 mm (9.50") | 89 mm (3.50") | 32 mm (1.25") | 6,000 PSI |
| PI-GRV-LE-08M08F-10K | 1/2" NPT Male | (3) 1/2" NPT Female | 102 mm (4.00") | 197 mm (7.75") | 98 mm (3.85") | 38 mm (1.50") | 10,000 PSI |
| Part No. | Inlet Size | Outlet Sizes | Lagging L1 (in) | Overall L (in) | Height H (in) | Hex Body (in) | Pressure Rating |
|---|---|---|---|---|---|---|---|
| PI-GRV-LE-08M08F-4 | 1/2" NPT M | (3) 1/2" NPT F | 4.00 in | 7.25 in | 3.50 in | 1.25 in | 6,000 PSI |
| PI-GRV-LE-08M08F-6 | 1/2" NPT M | (3) 1/2" NPT F | 6.00 in | 9.25 in | 3.50 in | 1.25 in | 6,000 PSI |
| PI-GRV-LE-12M08F-4 | 3/4" NPT M | (3) 1/2" NPT F | 4.00 in | 7.50 in | 3.50 in | 1.25 in | 6,000 PSI |
| PI-GRV-LE-12M08F-6 | 3/4" NPT M | (3) 1/2" NPT F | 6.00 in | 9.50 in | 3.50 in | 1.25 in | 6,000 PSI |
| PI-GRV-LE-08M08F-10K | 1/2" NPT M | (3) 1/2" NPT F | 4.00 in | 7.75 in | 3.85 in | 1.50 in | 10,000 PSI |
| Operating Parameter | Standard Specification | Severe Service / High-Pressure Rating |
|---|---|---|
| Maximum Operating Pressure | Up to 6,000 PSI (414 Bar) cold working pressure | Up to 10,000 PSI (690 Bar) with forged body |
| Hydrostatic Shell Test Pressure | 1.5 × Working Pressure (9,000 PSI / 621 Bar) | 1.5 × Working Pressure (15,000 PSI / 1,035 Bar) |
| Pneumatic Seat Test Pressure | 1,000 PSI (70 Bar) Nitrogen Gas Test | Zero Bubble Leakage Rate per API 598 |
| Working Temperature Range | -54°C to 204°C (-65°F to 400°F) with PTFE | -54°C to +538°C (1,000°F) with High-Purity Grafoil |
| Stem Tip Construction | Hardened non-rotating stem tip (axial closure) | Stellite 6 hard-faced / 17-4PH hardened |
| Integral Backseat Sealing | Metal-to-metal backseat isolates packing in open position | Prevents stem blowout and fugitive emissions |
| Design & Quality Standards | ASME B16.34, ASME B31.3, MSS-SP-99, MSS-SP-105 | NACE MR0175 / ISO 15156 Sour Gas Service |
| Inspection Certification | EN 10204 Type 3.1 Mill Test Certificate | 100% Raw Material Heat Traceability |
Pioneer Industries manufactures Stainless Steel Lagging Extension Gauge Root Valve using premium ASTM A182 / ASTM A479 high-tensile stainless steel and exotic alloys:
| Component / Grade | Material Standard | Composition / Engineering Feature |
|---|---|---|
| Body & Extended Shank | ASTM A182 Grade F316 / F316L (UNS S31600 / S31603) | Cr 16.0-18.0%, Ni 10.0-14.0%, Mo 2.0-3.0%, C ≤ 0.03% |
| Valve Bonnet | ASTM A182 Grade F316 / F316L Screwed Bonnet | Anti-vibration safety locking pin mechanism |
| Valve Stem | ASTM A479 Type 316 / 17-4PH Stainless Steel | High-tensile burnished stem with rolled threads |
| Non-Rotating Tip | Hardened 17-4PH Stainless Steel / Stellite 6 | Pure linear axial closure without rotational scoring |
| Stem Packing | Virgin PTFE (Standard) / High-Purity Grafoil | Live-loaded multi-ring packing for zero fugitive emissions |
| T-Bar Handle | AISI 304 Stainless Steel with Lock Screw | Ergonomic high-leverage operating handle |
Our manufacturing, machining tolerances, and quality verification strictly adhere to international engineering benchmarks:
Stainless Steel Lagging Extension Gauge Root Valve components are deployed across critical fluid systems requiring reliable primary process isolation, high working pressure up to 6,000 PSI, and multiport instrument hookups.
Penetrates 100mm+ mineral wool lagging on high-temperature steam lines, providing safe isolation for boiler pressure gauges and transmitters.
Allows close-coupled instrument mounting on hot fractionator columns and towers without requiring cutout damage to insulation jackets.
High-temperature Grafoil packing withstands thermal radiation while the extended shank maintains the handle at safe operating temperatures.
Eliminates fabricated pipe nipples and tees, offering corrosion-resistant 316SS block, bleed, and calibration access on black liquor lines.
Multiport outlet configuration allows mounting the primary transmitter alongside a calibration test port on jacketed hot chemical reactors.
Marine-grade 316/316L stainless steel provides marine corrosion resistance on insulated offshore topside flare and fuel gas headers.
Pioneer Industries’ Stainless Steel 2-Way Ball Valve Tube to Tube components are trusted across critical global industries for severe service reliability.
Explore technical engineering insights regarding pressure ratings, thermal insulation standoff, materials, and multiport installations.
A Stainless Steel 2-Way Ball Valve Tube to Tube features integrated double ferrule compression tube fittings machined directly into both ends of the valve body. When tightening the compression nut 1-1/4 turns past finger-tight, the front ferrule is driven into the body cone and swaged onto the tube outer diameter to create a 100% gas-tight metal-to-metal seal. Simultaneously, the case-hardened back ferrule advances, burnishing and colleting the tube wall to provide strong mechanical grip and vibration resistance without weakening the tubing.
Integrated tube ends eliminate two intermediate NPT/BSPP threaded joints, reducing potential leak points, eliminating thread sealant (PTFE tape or paste) which can break loose and clog sensitive analyzer orifices, saving substantial envelope length, and decreasing installation labor by up to 50% on instrumentation panels.
Yes. Our double ferrule compression geometry is engineered to be fully intermixable and interchangeable with major international tube fitting manufacturers (including Swagelok, Parker A-LOK, and Hoke Gyrolok), adhering strictly to global instrumentation tubing dimensional and performance standards.
Pioneer Industries manufactures tube-to-tube ball valves for fractional tubing from 1/8" to 1" O.D. and metric tubing from 6mm to 25mm O.D. Working pressures reach up to 500 Bar (6,000 PSI / optional 10,000 PSI series), with pressure holding capability matching or exceeding the burst pressure of heavy-wall ASTM A269 316/316L tubing.
For optimal sealing, use high-quality fully annealed seamless ASTM A269 or ASTM A213 Grade 316/316L stainless steel tubing with a maximum hardness of Rockwell HRB 90 (or 200 HV). Tubing must be clean, scratch-free, and within outer diameter tolerances of ±0.005" (±0.13mm).
Yes. Our tube-to-tube valves are equipped with external body threads and heavy-duty stainless steel panel mounting nuts. This allows clean, rigid pass-through mounting through instrument panels, analyzer shelters, and DCS consoles up to 12mm panel thickness without straining connected tubing lines.
Pioneer Industries double ferrule fittings can be disassembled and remade more than 25 times without loss of leak integrity. For reassembly, insert the tubing until the front ferrule seats in the body, tighten the nut hand-tight, then advance the nut approximately 1/4 turn with an open-end wrench (or until a sharp rise in torque is felt).
After initial makeup (1-1/4 turns from finger-tight for sizes > 3/16"), an inspector attempts to slide a standard gap inspection gauge between the nut and the valve body hex shoulder. If the gauge cannot enter the gap, the fitting is correctly tightened. If the gauge slides into the gap, further tightening is required to complete ferrule swaging.
For analytical gas chromatography and ultra-pure sampling, we supply Virgin PTFE or Modified PCTFE seats with electropolished 316 ball trims. When tested with mass spectrometer helium leak detectors, Pioneer Industries tube ball valves exhibit leakage rates below 1 x 10⁻⁹ sccs, ensuring zero atmospheric ingress.
All valves are dispatched with EN 10204 3.1 material test certificates, hydrostatic test reports, and raw material heat traceability. Each tube end is capped with protective polyethylene plugs to protect precision ferrule cones and threads, individually poly-bagged, and packed in heavy-duty export crates.
about your requirement to select the right products for your application needs!
Do you have any questions or need help with our services and products? Submit an Enquiry Form request or Call us at 9821023876. Feel free to get in touch!
Note: Please note that the information on this document is for illustration purposes only as information may vary with individual products, their grade and applications industries or uses and therefore cannot be guaranteed as accurate. © Copyright 2026 by Pioneer Industries. All Rights Reserved.