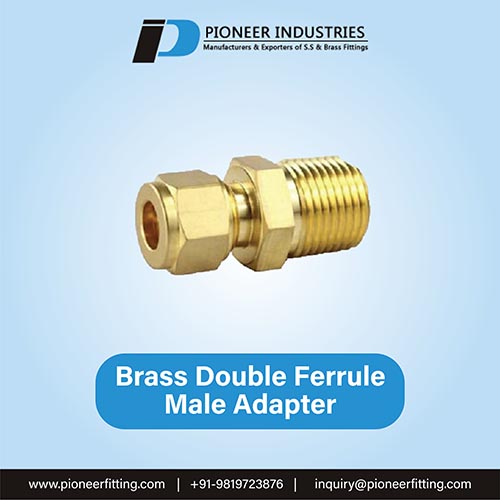
Engineered to provide a permanent, leak-proof transition from fractional or metric instrumentation tubing to welded piping headers, Pioneer Industries Brass Double Ferrule Male Pipe Weld Connectors combine mechanical compression reliability with robust weld joint integrity.
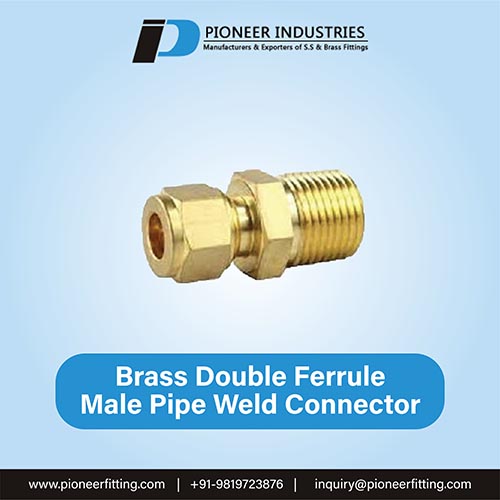
The Brass Double Ferrule Male Pipe Weld Connector creates a permanent, high-integrity bridge between fractional or metric tubing systems and heavy-wall welded pipe headers. One end features a precision-machined twin-ferrule compression port, while the opposing end is machined to standard pipe weld schedules for socket or butt welding.
Manufactured from high-grade brass bar stock conforming to ASTM B16 CW614N or forged brass ASTM B283, this connector provides superior thermal dissipation and structural strength, ensuring zero distortion of the internal ferrule seating surfaces during welding or brazing operations.
Supplied globally by Pioneer Industries Mumbai to petrochemical refineries, offshore platforms, gas chromatography labs, and heavy equipment builders requiring rigid, vibration-proof piping tie-ins.
Components are precision CNC-machined from premium extruded brass (IS 319 / ASTM B16 / CW614N) with micro-smooth surface finishes. Every production lot undergoes rigorous metallurgical spectrometry, optical CMM dimensional checks, and helium leak detection, accompanied by authentic EN 10204 Type 3.1 Mill Test Certificates.
To Get Quotes within hour Call Us at 9821023876 or Send Enquiry for the products you requires
Pioneer Male Pipe Weld Connectors are machined to tight dimensional tolerances per ASME B31.3 and B16.11, featuring beveled or socket-prep weld ends that ensure uniform heat distribution and complete weld penetration.
The compression fitting end utilizes our dual-ferrule mechanical swaging geometry, isolating the tubing from line vibrations and thermal contraction stresses common in process skids.
Metric tubing sizes 6 mm to 25 mm OD (MPMCW Series) and fractional sizes 1/8" to 1" OD (IPMCW Series) with weld pipe sizes from 1/8" to 1" NB.
Explore comprehensive engineering dimensional configurations for Metric Series and Fractional Series, Operating Parameters, and Certified Metallurgy. Manufactured according to ASME B31.3, ISO 19879, and international instrumentation standards.
| Part No. | Tube O.D. T mm | Pipe Weld Size P mm | E mm | h mm | H mm | F | G | l | l | L | Working Pressure |
|---|---|---|---|---|---|---|---|---|---|---|---|
| MPMWC-03-02 | 3 | 1/8 | 2.4 | 12 | 12 | 12.9 | 15.3 | 23.1 | 9.7 | 29.7 | 5,000 PSI / 345 Bar |
| MPMWC-04-02 | 4 | 1/8 | 2.4 | 12 | 12 | 13.7 | 16.1 | 24.1 | 9.7 | 30.7 | 5,000 PSI / 345 Bar |
| MPMWC-06-02 | 6 | 1/8 | 4.8 | 14 | 14 | 15.3 | 17.7 | 25.4 | 9.7 | 32.8 | 5,000 PSI / 345 Bar |
| MPMWC-06-04 | 6 | 1/4 | 4.8 | 14 | 14 | 15.3 | 17.7 | 30.2 | 14.2 | 37.6 | 5,000 PSI / 345 Bar |
| MPMWC-08-02 | 8 | 1/8 | 5.1 | 15 | 16 | 16.2 | 18.6 | 26.7 | 9.7 | 34.2 | 5,000 PSI / 345 Bar |
| MPMWC-08-04 | 8 | 1/4 | 6.4 | 15 | 16 | 16.2 | 18.6 | 31.2 | 14.2 | 38.7 | 5,000 PSI / 345 Bar |
| MPMWC-08-08 | 8 | 1/2 | 6.4 | 22 | 16 | 16.2 | 18.6 | 37.3 | 19.0 | 44.8 | 5,000 PSI / 345 Bar |
| MPMWC-10-04 | 10 | 1/4 | 7.1 | 18 | 19 | 17.2 | 19.5 | 33.3 | 14.2 | 40.9 | 5,000 PSI / 345 Bar |
| MPMWC-10-06 | 10 | 3/8 | 7.9 | 18 | 19 | 17.2 | 19.5 | 32.5 | 14.2 | 40.1 | 5,000 PSI / 345 Bar |
| MPMWC-10-08 | 10 | 1/2 | 7.9 | 22 | 19 | 17.2 | 19.5 | 38.1 | 19.0 | 45.7 | 5,000 PSI / 345 Bar |
| MPMWC-12-04 | 12 | 1/4 | 7.1 | 22 | 22 | 22.8 | 22.0 | 33.3 | 14.2 | 43.4 | 5,000 PSI / 345 Bar |
| MPMWC-12-06 | 12 | 3/8 | 9.5 | 22 | 22 | 22.8 | 22.0 | 33.3 | 14.2 | 43.4 | 5,000 PSI / 345 Bar |
| MPMWC-12-08 | 12 | 1/2 | 9.5 | 24 | 22 | 22.8 | 22.0 | 38.1 | 19.0 | 48.2 | 5,000 PSI / 345 Bar |
| MPMWC-15-08 | 15 | 1/2 | 11.9 | 24 | 25 | 24.4 | 22.0 | 38.9 | 19.0 | 49.0 | 5,000 PSI / 345 Bar |
| MPMWC-16-08 | 16 | 1/2 | 12.7 | 24 | 25 | 24.4 | 22.0 | 38.9 | 19.0 | 49.0 | 5,000 PSI / 345 Bar |
| MPMWC-18-08 | 18 | 1/2 | 13.5 | 27 | 30 | 24.4 | 22.0 | 40.4 | 19.0 | 50.05 | 5,000 PSI / 345 Bar |
| Part No. | Tube O.D in | Pipe Weld Size P Nom | Pipe Weld Size O.D Min | E Min | h | H | F | G | l | l | L | Working Pressure |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| RIPMWC-02-02 | 1/8 | 1/8 | 10.30 | 2.28 | 7/16 | 7/16 | 12.70 | 15.24 | 23.87 | 9.65 | 31.24 | 5,000 PSI / 345 Bar |
| IPMWC-03-02 | 3/16 | 1/8 | 10.30 | 3.04 | 7/16 | 1/2 | 13.71 | 16.0 | 24.63 | 9.65 | 31.24 | 5,000 PSI / 345 Bar |
| RIPMWC-04-02 | 1/4 | 1/8 | 10.30 | 4.82 | 1/2 | 9/16 | 15.24 | 17.78 | 25.40 | 9.65 | 32.76 | 5,000 PSI / 345 Bar |
| RIPMWC-04-04 | 1/4 | 1/4 | 13.70 | 4.82 | 9/16 | 9/16 | 15.24 | 17.78 | 30.48 | 14.22 | 37.84 | 5,000 PSI / 345 Bar |
| RIPMWC-05-02 | 5/16 | 1/8 | 10.30 | 5.08 | 9/16 | 5/8 | 16.25 | 18.54 | 26.67 | 9.65 | 37.03 | 5,000 PSI / 345 Bar |
| RIPMWC-05-04 | 5/16 | 1/4 | 13.70 | 6.35 | 9/16 | 5/8 | 16.25 | 18.54 | 31.24 | 14.22 | 38.60 | 5,000 PSI / 345 Bar |
| IPMWC-06-04 | 3/8 | 1/4 | 13.70 | 7.11 | 5/8 | 11/16 | 16.76 | 19.30 | 32.51 | 14.22 | 39.87 | 5,000 PSI / 345 Bar |
| IPMWC-06-06 | 3/8 | 3/8 | 17.10 | 7.11 | 11/16 | 11/16 | 16.76 | 19.30 | 32.51 | 11.05 | 39.87 | 5,000 PSI / 345 Bar |
| IPMWC-06-08 | 3/8 | 1/2 | 21.30 | 7.11 | 7/8 | 11/16 | 16.76 | 19.30 | 38.86 | 14.22 | 43.23 | 5,000 PSI / 345 Bar |
| IPMWC-08-06 | 1/2 | 3/8 | 17.10 | 10.41 | 13/16 | 7/8 | 22.86 | 21.84 | 33.27 | 19.05 | 43.43 | 5,000 PSI / 345 Bar |
| RIPMWC-08-08 | 1/2 | 1/2 | 21.30 | 10.41 | 7/8 | 7/8 | 22.86 | 21.84 | 38.86 | 14.22 | 49.02 | 5,000 PSI / 345 Bar |
| RIPMWC-08-12 | 1/2 | 3/4 | 26.67 | 10.41 | 1-1/16 | 7/8 | 22.86 | 21.84 | 40.38 | 19.05 | 50.54 | 5,000 PSI / 345 Bar |
| RIPMWC-10-08 | 5/8 | 1/2 | 21.30 | 12.70 | 15/16 | 1 | 24.38 | 21.84 | 38.66 | 19.05 | 49.02 | 5,000 PSI / 345 Bar |
| RIPMWC-12-12 | 3/4 | 3/4 | 26.67 | 15.74 | 1-1/16 | 1-1/8 | 24.38 | 21.84 | 40.38 | 19.05 | 50.54 | 5,000 PSI / 345 Bar |
| RIPMWC-16-16 | 1 | 1 | 33.40 | 22.35 | 1-3/8 | 1-1/2 | 31.24 | 26.41 | 50.03 | 23.87 | 62.23 | 5,000 PSI / 345 Bar |
| Operating Parameter | Standard Specification | Severe Service / High-Pressure Rating |
|---|---|---|
| Fluid Media Compatibility | Compressed Air, Mineral Oils, Hydraulic Fluids, Inert Gases | Natural Gas, Vacuum lines, Steam & Glycol circuits |
| Working Pressure Range | Vacuum to 5,000 PSI (345 Bar) depending on tube size | Proof pressure tested to 1.5× design working pressure |
| Helium Leak Integrity | < 1 × 10⁻⁹ mbar·l/s | Suitable for ultra-clean analytical & vacuum systems |
| Temperature Envelope | -200°C to +200°C (-328°F to +392°F) | Cryogenic to moderate steam and hot oil service |
| Turns From Finger-Tight | 1-1/4 Turns (sizes 1/4" to 1" / 6mm to 25mm) | 3/4 Turn (sizes 1/16" to 3/16" / 2mm to 4mm) |
| Compatible Tubing | Seamless Copper (ASTM B75, B88), Brass (ASTM B135) | Nylon, PU, PTFE (with Pioneer brass tube inserts) |
Pioneer Industries manufactures Brass Double Ferrule Male Pipe Weld Connector using high-tensile extruded brass bar stock and forgings with controlled microstructural annealing:
| Component / Grade | Material Standard | Composition / Chemistry |
|---|---|---|
| Fitting Body / Bar | ASTM B16 / IS 319 Gr. 1 / CW614N | Cu: 60.0–63.0%, Pb: 2.5–3.7%, Fe: 0.35% Max, Zn: Balance |
| Forged Elbows / Tees | ASTM B283 / CW617N C37700 | Cu: 57.0–60.0%, Pb: 1.5–2.5%, Fe: 0.30% Max, Zn: Balance |
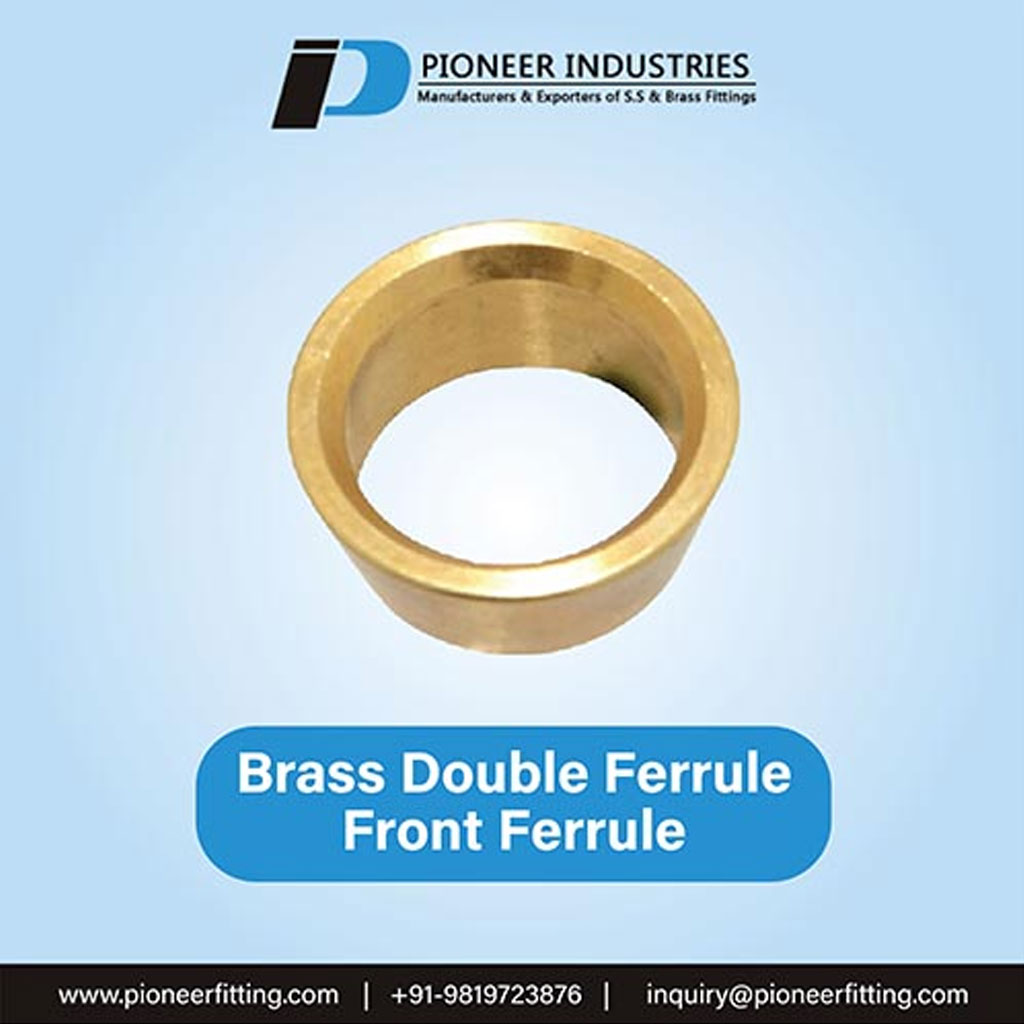
| Front & Back Ferrules | ASTM B16 / Cold-Worked Annealed | Controlled Alpha-Beta phase balance for clean collet swaging |
| Optional Naval Brass | ASTM B21 / CW712R C46400 | Cu: 59.0–62.0%, Sn: 0.5–1.0%, Pb: 0.20% Max, Zn: Balance |
Our manufacturing, swaging tolerances, and quality verification strictly adhere to international engineering benchmarks:
Brass Double Ferrule Male Pipe Weld Connector components are deployed across demanding industrial instrumentation, process lines, and pneumatic circuits, including:
Transitioning from welded steam or cooling headers to flexible copper or brass tubing lines.
Withstanding severe cyclic vibration at reciprocating gas compressor manifold connections.
Welding directly into primary process sample probes for rigid sample extraction lines.
Providing permanent structural piping connections with demountable instrument take-offs.
Eliminating potential leak paths at header joints in semiconductor and laboratory gas manifolds.
Connecting tubing impulse lines to heavy welded boiler drum tapings.
Rigid welding into return line tanks and pressure distribution blocks.
Resisting salt air corrosion and high-velocity steam vibration on marine auxiliary boards.
Pioneer Industries’ Brass Double Ferrule Male Pipe Weld Connector components are trusted across critical global industrial sectors:
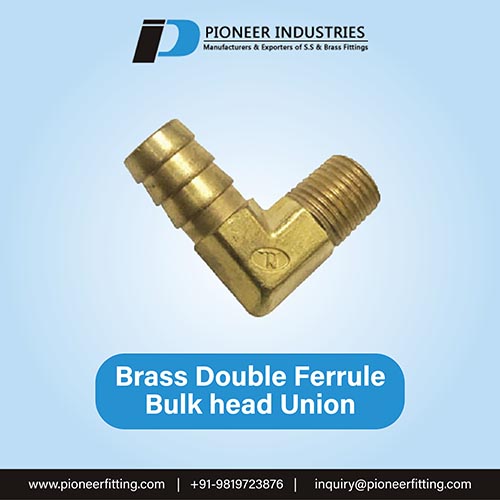
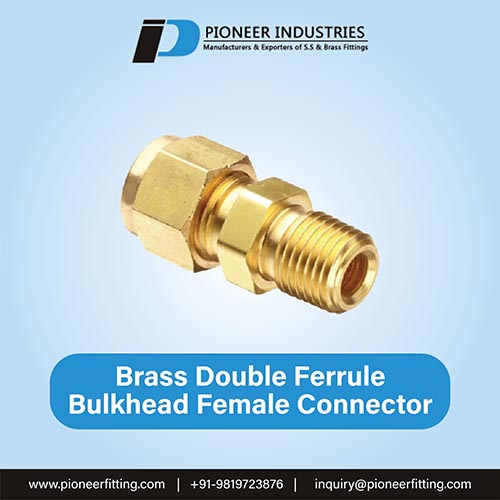
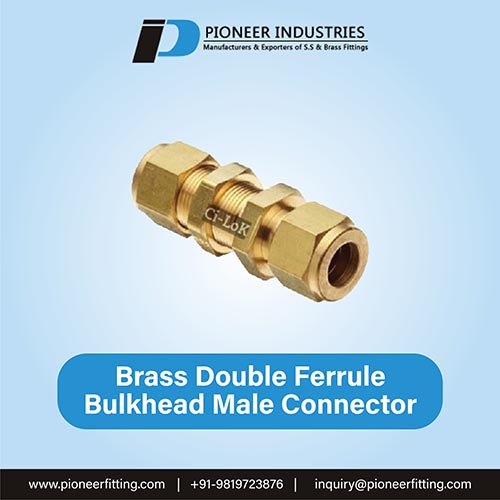
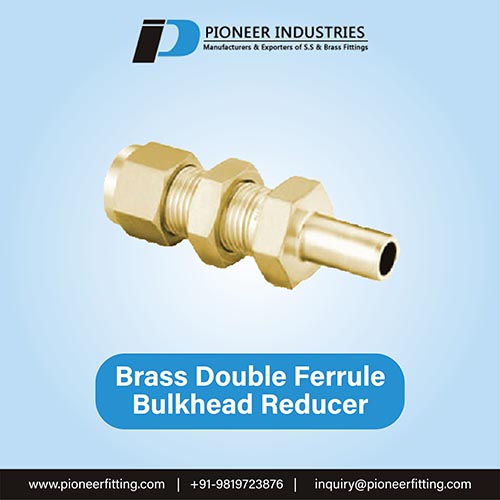
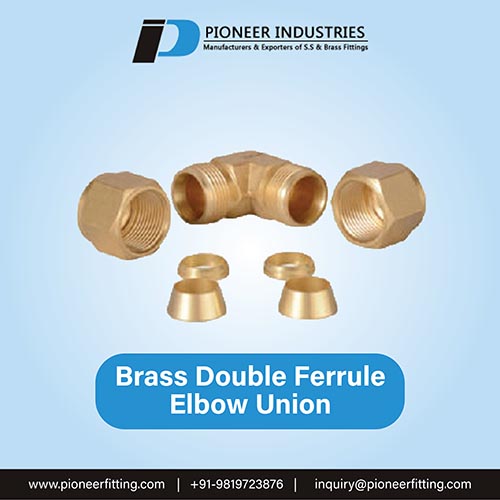
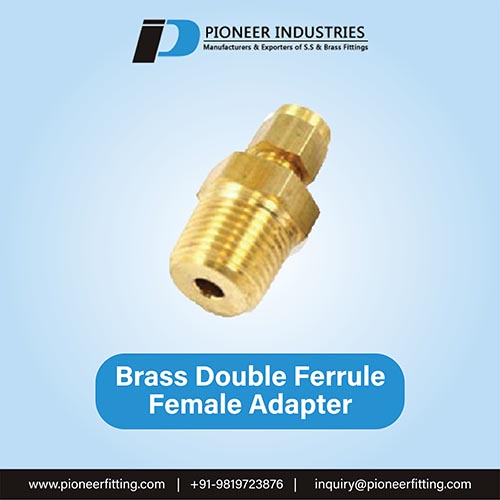
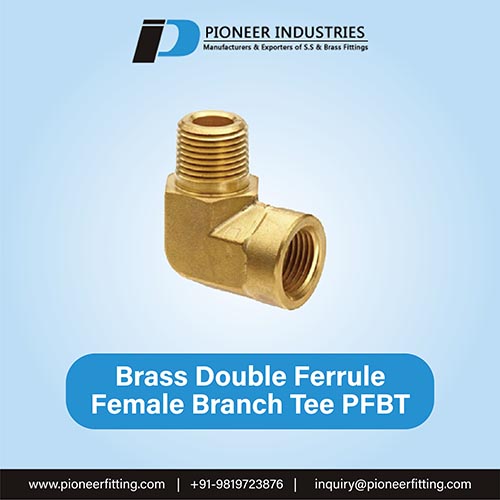
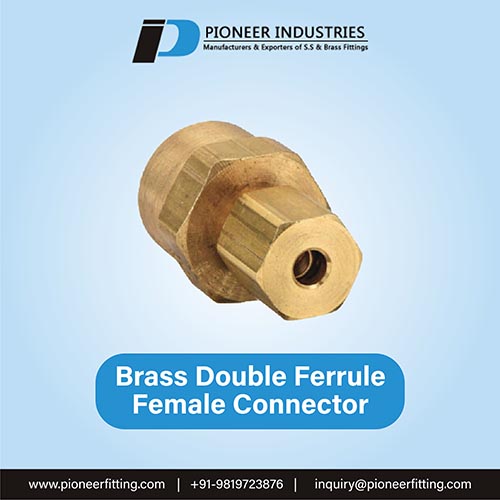
Expert engineering insights and technical guidance regarding swaging mechanics, pressure thresholds, tubing compatibility, and installation protocols for Brass Double Ferrule Male Pipe Weld Connector.
A Brass Double Ferrule Male Pipe Weld Connector is a specialized transition fitting featuring a double-ferrule compression tube connection on one end and a male pipe weld stub (socket or butt weld) on the other, joining tubing to welded piping headers.
The pipe weld end is machined with standard pipe bevels or socket-weld counterbores. In brass systems, joining is typically accomplished via silver brazing or specialized TIG welding using matching copper-alloy filler rods.
To protect the precision internal ferrule seat, disassemble the nut and ferrules prior to welding. Apply heat sinks or wet rags around the fitting body during brazing, and inspect the cone surface before reassembling the tube.
Metric Series MPMCW covers 6mm to 25mm tube OD, and Fractional Series IPMCW covers 1/8″ to 1″ tube OD with pipe weld stubs from 1/8″ to 1″ nominal pipe size (Schedule 40/80).
Rated up to 5,000 PSI (345 Bar) on the compression tube side for sizes 1/8″ to 1/4″ and up to 3,200 PSI for 1/2″, fully matching the working pressure rating of heavy-wall brass tubing.
Manufactured from extruded brass bar stock conforming to ASTM B16 Alloy C36000 or forged brass ASTM B283 CW617N / C37700.
Insert the tube squarely to the internal shoulder, hand-tighten the nut, and then tighten 1-1/4 turns with an open-end wrench (3/4 turn for sizes 1/8″ and 3/16″).
Yes. The double-ferrule swaged joint can be repeatedly remade without compromising sealing integrity by tightening approx. 1/12 to 1/6 turn past finger snug.
Yes, precision twin-ferrule mechanical swaging ensures vacuum sealing down to 1 × 10⁻⁹ mbar·l/s.
Every production lot includes EN 10204 Type 3.1 Material Test Certificates, chemical/mechanical analysis, and hydrostatic pressure test verification.
about your requirement to select the right products for your application needs!
Do you have any questions or need help with our services and products? Submit an Enquiry Form request or Call us at 9821023876. Feel free to get in touch!
Note: Please note that the information on this document is for illustration purposes only as information may vary with individual products, their grade and applications industries or uses and therefore cannot be guaranteed as accurate. © Copyright 2026 by Pioneer Industries. All Rights Reserved.